From Measurement to Control: Improving Process Capability in Medical Device Manufacturing
 Consistency is critical in medical device manufacturing. But achieving it takes more than inspecting finished parts.
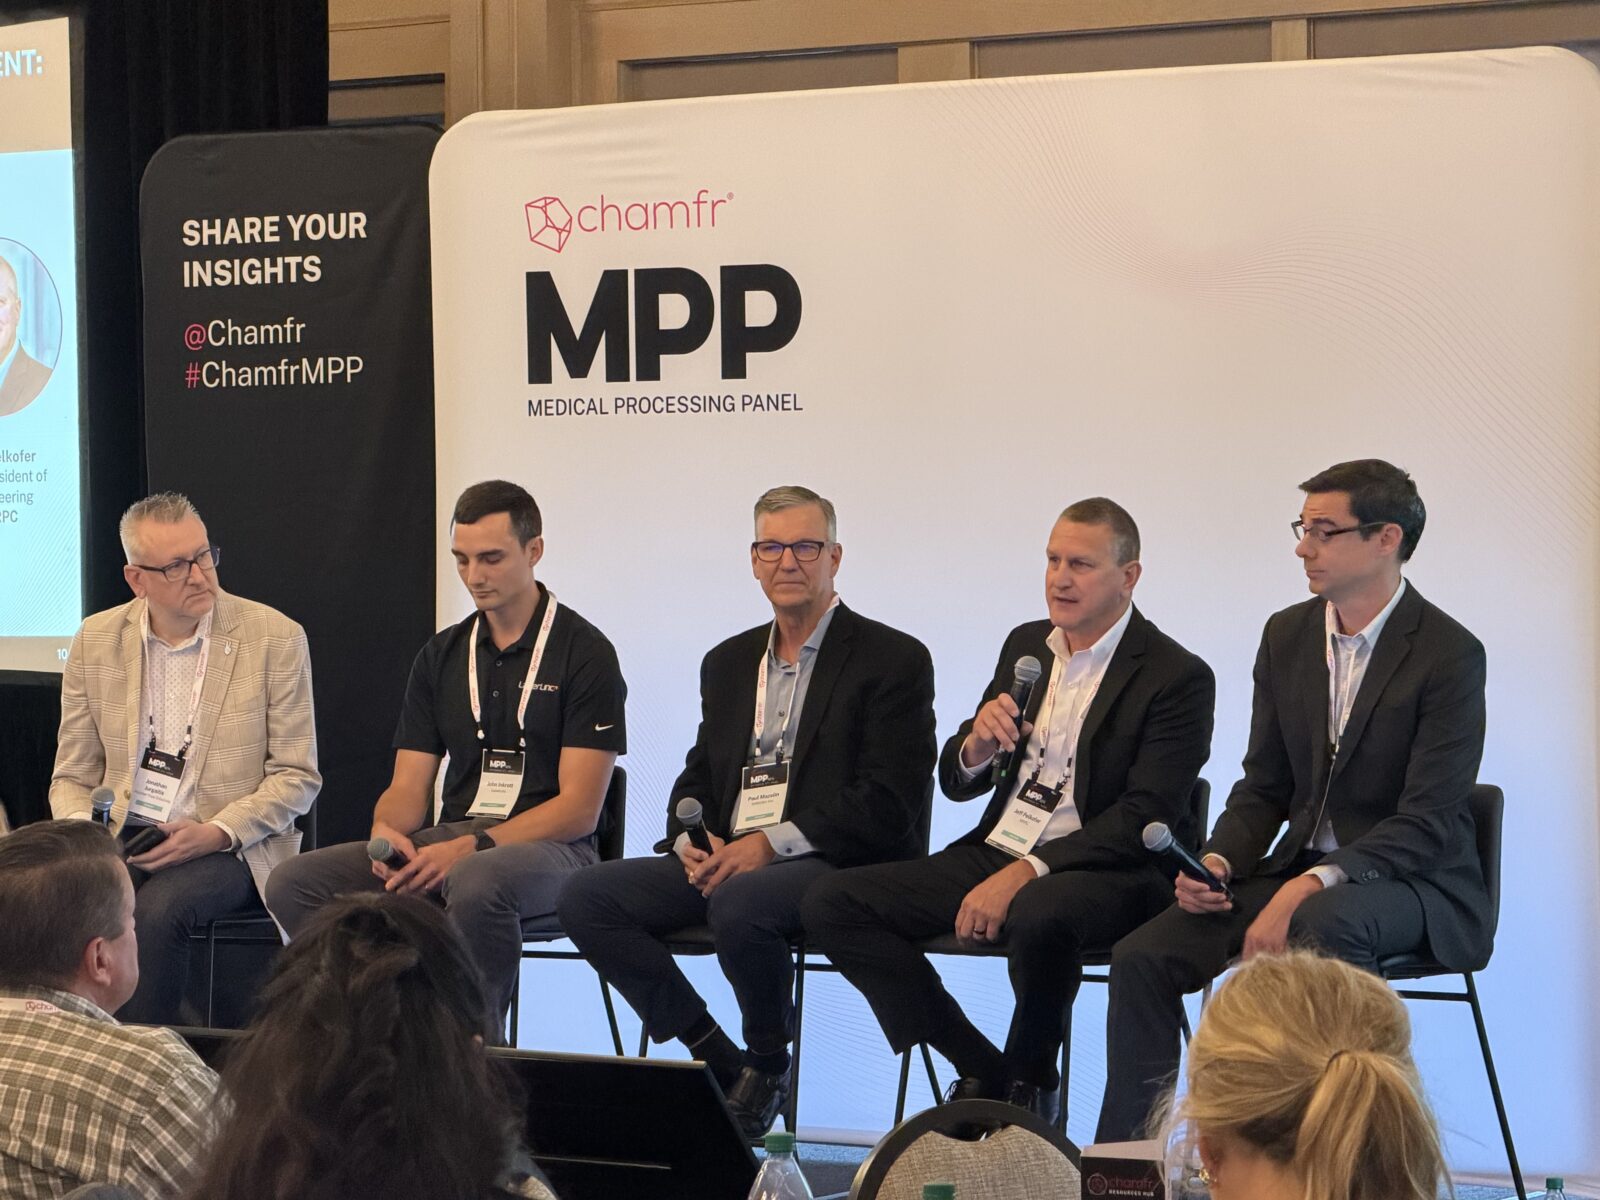
At MPP Minnesota 2026, MRPC Vice President of Engineering Jeff Pelkofer joined industry experts for a panel discussion on Polymer Processing & In-Process Measurement: Improving Yield & Process Capability. The conversation explored how manufacturers are using in-process measurement, cavity-pressure sensing, vision systems, closed-loop control and advanced metrology to better understand and control their processes.
For medical device manufacturers, the opportunity is significant: identify variation earlier, understand what is actually driving it, and use that information to build more consistent processes.
Start With the Part, Not the Inspection
Before deciding how a component should be measured or inspected, manufacturers need to understand what the part actually needs to do.
That means looking at the design, material, tooling and process together. Just as importantly, it means understanding how the customer will use the finished component.
“Communication is key. We’ve got to go to our customer and make sure that we fully understand how they intend to use that product, that part. And the more we can understand from them and what their need or want is, the better we can work with them to improve their design.”
That early collaboration can help manufacturers determine which characteristics are truly critical, which tolerances are realistic, and what level of inspection is actually necessary.
“You’ve got to have a good design, you’ve got to have a good mold, and you’ve got to have a good process.”
Move Measurement Into the Process
Traditional inspection provides valuable information, but it happens after the part has already been molded. At that point, a problem may already mean scrap or a shift in tolerance that could affect production.
“Your part’s already molded, so if you run into a problem at that point, you’ve already got scrap, or you’ve got a shift in your tolerance, hopefully you’re still in spec.”
In-process technologies such as cavity-pressure sensing offer another approach. Rather than waiting for downstream inspection to reveal a problem, manufacturers can monitor what is happening during the molding cycle and use that information to evaluate consistency from shot to shot.
“With this technology, we can monitor every shot and make sure that we’re getting the same part every time.”
Cavity pressure can also provide insight into changes in material behavior. Variations in material viscosity, for example, can change the pressure required to fill and pack a cavity. Monitoring that pressure provides another way to understand whether the molding process is producing a consistent component.
“Cavity pressure equals constant parts shot after shot.”
And the next step is moving beyond monitoring to actually controlling the process.
The Value of Closing the Loop
The panel discussion highlighted an important distinction: collecting process data is not the same as using it to control the process. Manufacturers can use measurement data to:
- Monitor process trends and identify variation
- Adjust processing conditions in response to changes
- Detect problems before large quantities of parts are produced
The goal is to move from simply monitoring a process to actively maintaining it. With the right controls in place, closed-loop systems can essentially “set the line on cruise control,” helping maintain consistency without relying solely on downstream inspection.
More Inspection Isn’t Always Better
It may seem logical that more inspection automatically means better quality. But the panel highlighted why that isn’t necessarily the case.
Early in a program, manufacturers often take a risk-averse approach because they don’t yet have enough historical data to understand where failures may occur. As the process matures, however, that data can provide evidence that certain inspections are no longer necessary.
One example discussed during the panel involved a program where inspections were removed after years of capability, validation and historical data supported the change. Five years later, the product had still experienced no failures or customer complaints following the reduction in inspection.
But when a next-generation version of the product was introduced, inspections were added back in. The reason?
“You have to follow the data.”
The lesson is that inspection strategies should evolve with the process. The goal isn’t to inspect everything. It’s to understand what matters and have the data to support the right inspection strategy.
Measure More During Development to Learn What Matters
That makes the development phase particularly important. During R&D, manufacturers can afford to measure more extensively and collect data across a wider range of process conditions. By correlating those process inputs with functional and performance results, teams can determine which characteristics actually have an impact on the finished product.
That information can then be used to “right size” production inspection, focusing resources on the characteristics that have demonstrated a meaningful relationship to product performance.
Beyond Dimensions: Looking for Attributes
Once dimensional characteristics are stable, the focus can shift to other attributes that can affect component quality, including:
- Particulate
- Flash
- Air bubbles
- Bonding and potential delamination in multi-material components
For high-volume programs, automated vision inspection can help manufacturers evaluate multiple dimensional and cosmetic characteristics while improving consistency and reducing reliance on manual inspection.
The challenge becomes even greater as medical components get smaller. Thin walls, tiny internal diameters and features measured in microns can push the limits of both manufacturing and metrology. A feature may be difficult to mold consistently, but it can be equally difficult to handle and accurately measure once it has been produced.
For thin-wall extrusion, factors such as gravity, head pressure, die swell and drawdown can all influence the final dimensions. The smaller and more precise the component, the more important it becomes to understand what is happening inside the process itself.
What’s Next: Predicting Variation Before It Happens
The evolution of process control doesn’t stop with monitoring and closed-loop adjustment. Looking ahead, technologies could use both process inputs and measurement outputs to predict what a process is likely to produce and make adjustments before an out-of-trend condition becomes an actual quality issue.
The common thread is clear: manufacturing is moving from reacting to variation toward anticipating it.
Connecting Design, Materials, Tooling and Process
Ultimately, the discussion at MPP Minnesota was about more than any single measurement technology.
Improving process capability starts with understanding the entire manufacturing system: the design, the material, the mold or tooling, the process, the measurement strategy and the function of the finished component.
At MRPC and across the combined organization, that connected approach brings together expertise in thermoplastic, silicone, multi-material and precision molding to help medical device manufacturers address those considerations earlier in development and throughout production.
The goal isn’t simply to measure more, it’s to understand more, control what matters, and build processes that consistently produce the component the custo